Cleaning Methods for the Compressor Side
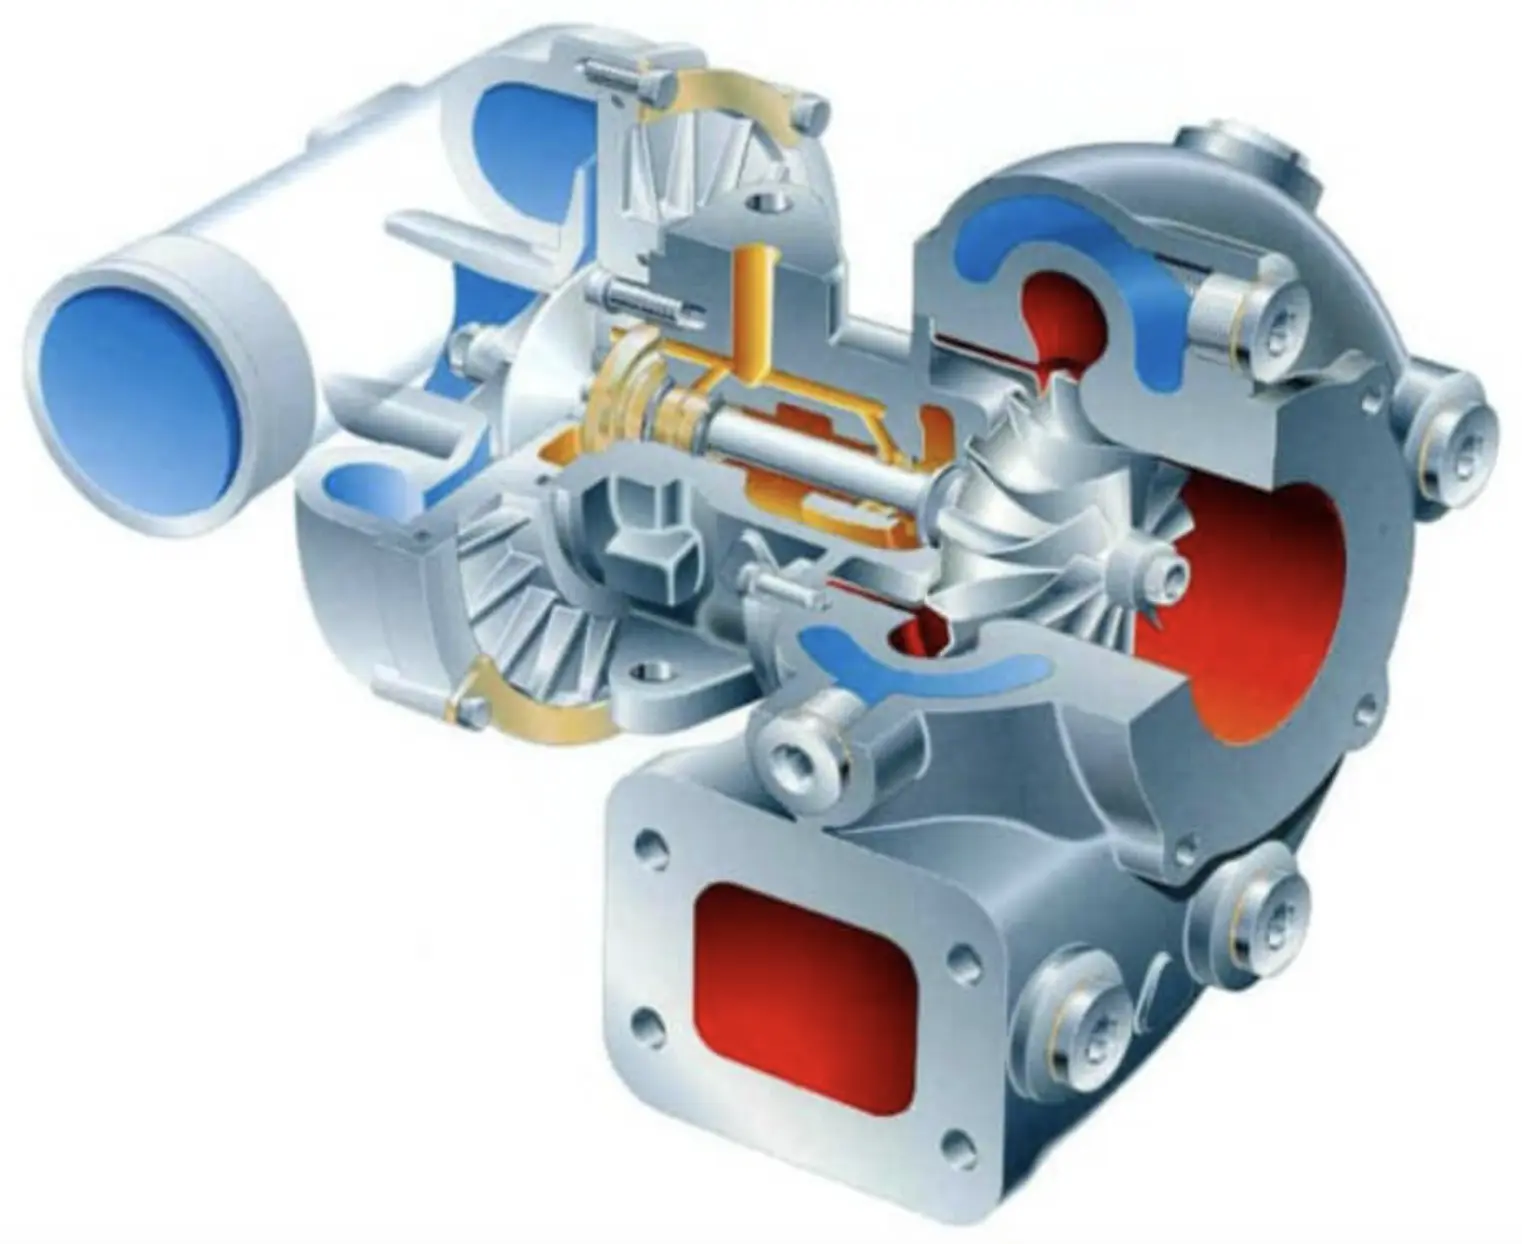
The compressor side of a marine turbocharger is cleaned primarily by water washing, a procedure performed while the engine is running. The method involves injecting clean fresh water into the compressor inlet, where the rotating compressor wheel atomizes the water into a fine mist. The water droplets dissolve water-soluble deposits and mechanically impact accumulated dirt, carrying it through the compressor and into the engine’s intake system, where it is burned or expelled.
The cleaning intervals and procedures vary by manufacturer, but certain principles are universal. ABB, a leading turbocharger manufacturer, recommends compressor wash-cleaning every 24 operating hours. The engine should be at normal operating temperature and the load should be as high as possible—that is, at high turbocharger speed—to maximise the cleaning effect. The cleaning procedure typically involves filling a water container with a measured quantity of clean fresh water, opening a shut-off valve for approximately three minutes, and then closing it. The water container should be emptied, and a successful cleaning is indicated by an increase in scavenge air pressure or a decrease in exhaust gas temperature.
MAN Energy Solutions specifies a similar procedure for its L21/31 engine, describing a water-washing system that removes dirt, salt, and oil build-up from turbocharger components by injecting a controlled flow of water while the engine is running at partial load. This is particularly valuable in marine and coastal operations where air contamination is high.
The water used for compressor washing must be clean and fresh. Salt water must never be used, as it would leave corrosive salt deposits on the compressor components. Cleaning agents are generally not added to the water for routine compressor washing, though proprietary cleaning fluids may be used in specific circumstances as directed by the manufacturer.
Cleaning Methods for the Turbine Side
Turbine-side cleaning is more complex and more critical than compressor cleaning. The deposits on the turbine side are primarily carbonaceous and result from the combustion of heavy fuel oil. They are harder, more tenacious, and more resistant to simple water washing than the deposits found on the compressor side. As a result, turbine cleaning typically employs a combination of methods: dry cleaning with granular material, water washing, and in some cases, steam cleaning.
Dry Cleaning
Dry cleaning, also known as nut-shell cleaning or soft blasting, involves injecting small, hard organic particles—typically ground nut shells or similar controlled-size granules—into the exhaust gas stream upstream of the turbine. These particles, carried by compressed air, impact the turbine blades and nozzle ring with a gentle abrasive action, dislodging carbon deposits without damaging the metal surfaces. Once they have done their work, the particles burn and disappear into the atmosphere through the stack, leaving no harmful residue.
The VECOM ASTEROIDS system is representative of this approach. The organic particles, with a controlled size of 1.3 to 1.7 mm, are blown by compressed air into the exhaust gas line before the gas inlet casing. A turbine should be cleaned every 24 to 48 hours of full-load operation, with cleaning repeated if the gas temperature after the turbine rises to 20°C above the normal temperature at full load. A key advantage of dry cleaning is that it can be performed at full engine load without reducing speed, unlike water washing, which requires a reduction in load to control exhaust gas temperatures.
For engines with multiple gas inlets or multiple turbochargers, each inlet and each turbocharger should be cleaned one after the other to ensure thorough coverage.
Water Washing
Water washing of the turbine side is used to remove deposits that dry cleaning alone cannot fully eliminate. Practical service experience has revealed that the turbine side of a turbocharger can only be sufficiently cleaned by a combination of dry cleaning and water washing. Water washing is typically performed at reduced engine load to keep the exhaust gas temperature at the turbine inlet below a safe threshold—usually 430°C for many turbocharger types—because injecting water into an excessively hot turbine can cause thermal shock and cracking.
The procedure involves connecting a water supply to a washing system that injects fresh water into the exhaust gas pipe before the turbine. The water is sprayed through a regulating valve, and the cleaning process is monitored by observing the exhaust gas temperature. A successful cleaning is indicated by a decrease in exhaust gas temperature and an improvement in turbocharger performance. Washing at intervals of 150 hours is recommended by MAN Energy Solutions for heavy fuel oil operation, though the exact interval depends on fuel quality and operating conditions.
Steam Cleaning
An alternative and increasingly sophisticated approach to turbine cleaning uses high-temperature, high-pressure steam. A patent filed by Harbin Engineering University describes a system in which steam is distributed through radially symmetrical nozzles in both the turbine and compressor casings. The high temperature of the steam vaporises oil and grease deposits, while the high pressure allows it to penetrate into narrow gaps and crevices more effectively than water or dry cleaning methods. The steam also carries thermal energy that can be transferred to the exhaust gas, improving the energy available to the turbine wheel and thereby enhancing turbocharger efficiency.
Steam cleaning offers the advantage of avoiding the chemical corrosion risks associated with water washing, particularly in the presence of sulphur residues. It is particularly effective for removing oily and greasy deposits that resist both dry and wet cleaning methods. However, steam cleaning systems require additional equipment and careful control of steam parameters, and they are not universally available on all vessels.
Maintenance of Bearings and Lubrication Systems
The turbocharger’s bearings are among its most critical and vulnerable components. At rotational speeds of 10,000 to 50,000 rpm or more, even a momentary interruption in lubrication can cause catastrophic failure. The case of a MAN B&W TCA66 turbocharger that suffered complete failure following a blackout illustrates the stakes. When the ship’s electrical system failed, the main lubricating oil pump stopped, and the emergency oil tank failed to supply adequate oil to the turbocharger bearings. The turbocharger continued to spin at approximately 10,000 rpm under its own inertia, but without lubrication, the bearing surfaces ground against each other, generating intense heat. The thrust bearing disc shattered into four pieces, the journal bearing was severely scored, and its inner diameter increased by 5 mm.
This incident underscores the importance of maintaining the turbocharger lubrication system in perfect condition. In normal operation, the turbocharger bearings receive oil from the main engine’s lubricating oil system, typically through a branch line with a flow-limiting orifice and a pressure-regulating valve. An emergency oil tank, mounted above the turbocharger, provides a gravity-fed oil supply in the event of a main pump failure. The emergency tank should be inspected regularly to ensure that its oil level is correct and that its supply passages are clear.
Regular maintenance of the lubrication system includes checking oil pressure and flow, inspecting oil filters and strainers, and verifying the operation of check valves and pressure regulators. Oil samples should be analysed periodically for signs of contamination, metal particles, or degradation. The emergency oil tank system, in particular, requires periodic testing to confirm that it will function when needed. A study of two marine turbocharger failures concluded that the emergency oil tank’s design and location can be improved—for example, by installing openable blind plates on the tank ends to facilitate cleaning and inspection, and by ensuring that the tank is positioned high enough to provide adequate gravity feed even as the oil level drops.
Scheduled Maintenance and Overhaul
Beyond routine cleaning, turbochargers require periodic inspection and overhaul to maintain reliability. ABB and other manufacturers recommend an overhaul every 10,000 to 15,000 working hours, or at least every two years, depending on operating conditions. Scheduled turbocharger reconditioning has been shown to improve engine fuel economy and performance while reducing exhaust emissions. A study analysing the effects of reconditioning on a marine diesel generator engine found that restoring proper clearances, alignment, and cleanliness in the turbocharger significantly improved engine efficiency and emissions formation.
The overhaul process involves dismantling the turbocharger, cleaning all components, measuring clearances, inspecting for wear and damage, replacing worn parts, and reassembling with correct tolerances. Critical measurements include the axial and radial clearances of the rotor shaft, the condition of the bearing surfaces, the wear on the turbine and compressor blades, and the integrity of sealing rings and gaskets. Components such as the turbine wheel and compressor wheel may require dynamic balancing after cleaning or repair to ensure smooth operation at high speed.
Recent developments in maintenance standards reflect the growing sophistication of the field. In China, the industry standard JT/T 283—2026, Technical Specifications for the Repair of Marine Internal Combustion Engine Turbochargers, was released by the Ministry of Transport and will take full effect in December 2026. This revision, the second since 1995, marks a significant advancement in the systematisation and refinement of turbocharger maintenance practices in the Chinese maritime industry.
Condition Monitoring and Fault Diagnosis
Effective maintenance is increasingly supported by condition monitoring and diagnostic techniques. Rather than relying solely on fixed time intervals, modern practice uses performance data to determine when cleaning or overhaul is actually needed. Key parameters to monitor include exhaust gas temperature before and after the turbine, scavenge air pressure, turbocharger speed, and air filter differential pressure.
Vibration analysis is a powerful diagnostic tool for turbocharger health. Abnormal vibration signatures can indicate bearing wear, rotor imbalance, blade damage, or fouling. Pressure and performance testing can reveal reductions in compressor efficiency or turbine power output. Oil analysis can detect bearing wear metals and lubricant degradation before a failure occurs. Computer-aided diagnostic systems are being developed that integrate these data streams to provide early warning of developing faults.
Regular visual checks are equally important. Inspecting the turbocharger for oil leaks, unusual noises, and vibration during operation can identify problems before they become serious. The air filter and silencer should be checked regularly and cleaned or replaced when differential pressure increases by 50% compared to the shop test value at the same engine load, or when the filter mat becomes discoloured.
Safety Considerations
Turbocharger cleaning and maintenance involve significant safety hazards that must be managed carefully. The turbine casing and exhaust gas piping operate at temperatures exceeding 400°C and can cause severe burns if touched. Rotating components continue to spin for several minutes after the engine is stopped and must not be approached until they have come to a complete standstill. When performing water washing, the water injection must be carefully controlled to avoid thermal shock to hot turbine components, and the exhaust gas temperature must be maintained below the manufacturer’s specified limit.
Personnel performing turbocharger maintenance should wear appropriate personal protective equipment, including heat-resistant gloves, safety glasses, and hearing protection. Lockout/tagout procedures must be followed to prevent accidental engine starting during maintenance. The turbocharger manufacturer’s instructions should always be consulted and followed precisely, as procedures and limits vary between models and applications.
Conclusion
The turbocharger is a marvel of engineering that transforms otherwise wasted exhaust energy into usable power, dramatically increasing the efficiency and output of marine diesel engines and generators. But this performance comes with a maintenance obligation. Carbon deposits, compressor fouling, bearing wear, and lubricant degradation all conspire to reduce turbocharger effectiveness and, by extension, engine reliability and fuel economy.
Regular cleaning—water washing of the compressor, combined dry and wet cleaning of the turbine—is the first line of defence. Proper maintenance of the lubrication system, including the emergency oil supply, protects against catastrophic bearing failure. Scheduled overhauls restore clearances and component condition to like-new standards. And condition monitoring, supported by vibration analysis, performance trending, and oil analysis, allows maintenance to be planned rather than reactive.
For the marine engineer, mastery of turbocharger cleaning and maintenance is a fundamental professional skill. The rewards are tangible: improved fuel economy, reduced emissions, longer component life, and the confidence that the engine will deliver reliable power when it is needed most. In an industry where every tonne of fuel and every hour of uptime matters, the turbocharger—and the engineer who maintains it—stands at the heart of operational excellence.